Improvement of the effectiveness of making alumina by the Updated ILTD Process: alumina refineries in India as examples (Part 1)
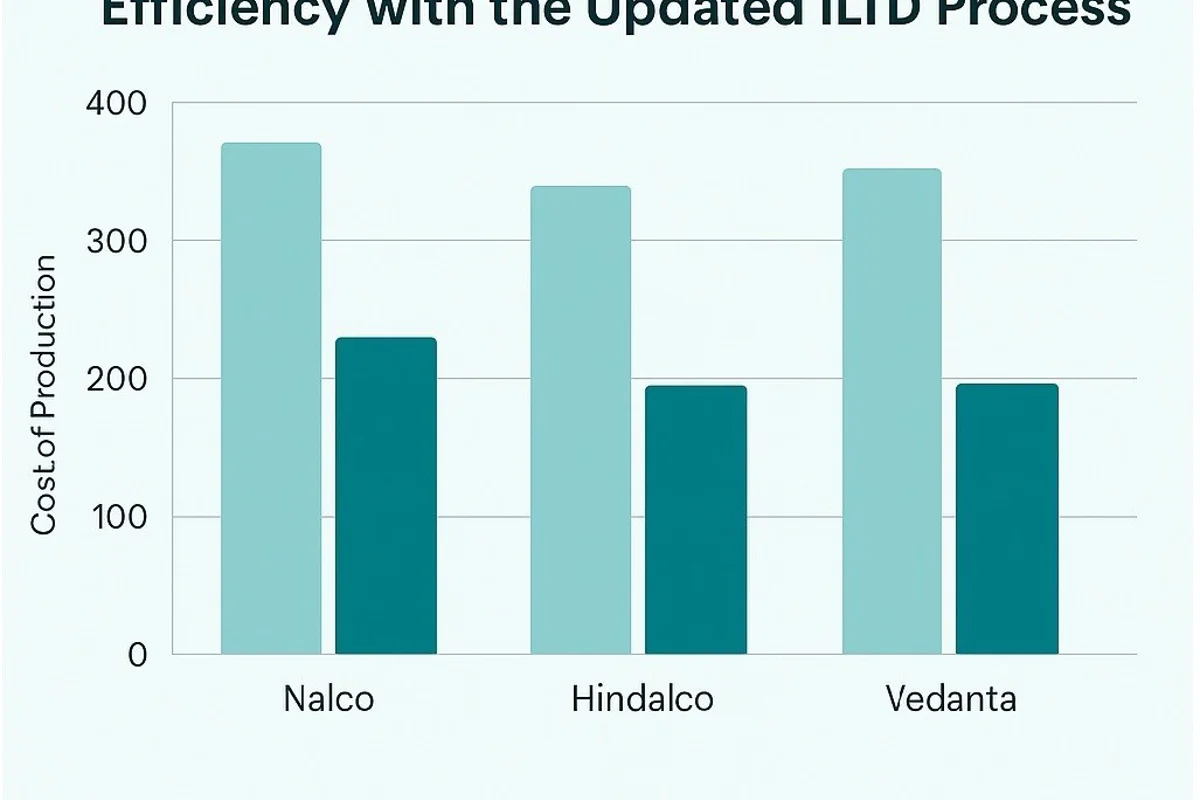
For those who are familiar with alumina production by the Bayer Process it is evident that that the Cost of Production (COP) largely depends on the Available alumina (A.Al) and Reactive silica (R.Si) content of the particular bauxite. The caustic consumption, which is mainly dependent on A.Al and R.Si; constitutes the second largest cost item after the cost of bauxite in the Bayer process.
Image for representational purpose
In India there are large lateritic bauxite resources with medium available alumina (trihydrated alumina, THA) and medium to high Reactive SiO2 content. With the deteriorating bauxite quality, refineries are struggling to keep the alumina production cost at the low level.
The Updated Improved Low Temperature Digestion (ILTD) Process as a novel way to increase the economic and environmental effectiveness of the alumina production is summarised in this paper.
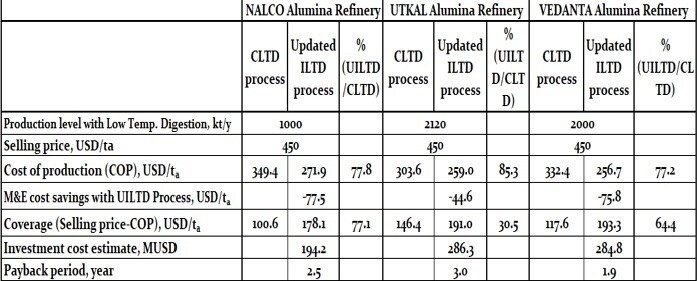
The approximate qualities of bauxite feedstocks, the production levels, and estimated unit costs were used for three alumina refineries located in the Eastern part of India. The Material and Energy consumptions, the amount and composition of bauxite residues, the same for the dicalcium-silicate (C2S) by-products were calculated and used to present the improvement in the COP of the Updated ILTD Process compared with the Conventional Low Temperature Digestion (CLTD). The coverage, i.e. difference of the Selling Price and the Cost of Production could be increased by 30, 64 and 77 per cent, respectively by the Updated ILTD Process. The Investment costs for the upgrade and the approximate Payback periods are estimated for each of the alumina refineries. For the three alumina refineries the Payback periods were found to be 1.9, 2.5 and 3 years, respectively, which are deemed to be good returns of investments. The aluminous laterites that are reasonably considered to be sub-economic materials for the Conventional Bayer Process are suitable for their viable processing with the Updated ILTD Process. In this case the Payback period was found to be low (1.3 years) „Bánvölgyi, G. (2021)”.
Although each of the unit operation that should be upgraded from the Conventional process have been or were on commercial scale operation, a pilot scale demonstration of the Updated ILTD Process is suggested so that commercialisation take place with maximum confidence. It may be noted that the alumina production process on similar line as ILTD process was sucessfully implemented in the Sumitomo refinery of Japan. The Sumitomo variant of the differential extraction process is now closed down, however, it is considered to be a proof of the concept.
Introduction
Over the decades there have been huge efforts made to reduce the Cost of Production by the Bayer Process, to develop process routes that make possible the viable processing of sub-economic bauxite resources, even aluminous laterites and introduce manufacturing alumina from gibbsitic bauxites that is not associated with the burden of harmful bauxite residue.
Case Studies proven that the Improved Low Temperature Digestion (ILTD) Process is suitable for viable processing of bauxites or aluminous laterites with relatively high Reactive Silica content „Bánvölgyi, G. and Nandi, A. (2022)”. The original ILTD Process was developed further and the Updated ILTD Process has been proposed recently. There is a limited scientific work on processing of high silica gibbsitic bauxite, which is now quite prevalent in India, Australia and other countries. This process requires moderate change of the existing digestion technology, however, the ILTD works with seeded post-desilication in place of pre-desilication.
World bauxite resources and the share of gibbsitic ores
Bárdossy and Aleva estimated the World bauxite resources to be 54 Gt, out of that 14 Gt was classified as sub-economic and hypothetical ores „Bárdossy, G. and Aleva, G.J.J. (1990)”. About 88 per cent of the bauxite resources are lateritic type. „The quantity of sub-economic and hypothetical resources could change considerably with further exploration and with further technological development.”(„Bárdossy, G. and Aleva, G.J.J. (1990)”) During 1997, the bauxite resources were estimated to be 75-100 Gt „Lyew-Ayee, Parris A. (1997)”. Komlóssy concluded that some 88-90 % of the reserves are of gibbsitic type ores, of which, about 5 % are mixed gibbsitic-boehmitic bauxites „Komlóssy, Gy. (2021)”.
ILTD and updated ILTD process
Fundamental considerations and principal features of the Improved Low Temperature Digestion (ILTD) Process
The dissolution reactions of gibbsite and kaolinite are best explained as a competition of gibbsite and kaolinite for the reactive OH- ions. In the gibbsitic bauxites gibbsite is present in a significantly larger amount (about 10-25 times higher than kaolinite), and, as kinetic studies have shown, has a higher dissolution reaction rate than that of kaolinite (about 10 times higher) during the Low Temperature Digestion. At low target reactive OH- concentrations (AH), gibbsite consumes most of the common reactant, the reactive OH- ions, before kaolinite totally dissolves. The reactive OH- concentration (AH) is defined as follows:
AH = 2 x 17 [(cAl2O3eq -c Al2O3)/102 – cSiO2/60] (g/L)
Where 17, 102 and 60 are the molar masses of OH, Al2O3 and SiO2, respectively. cAl2O3eq is the equilibrium solubility for gibbsitic alumina, cAl2O3 and cSiO2 are dissolved alumina and silica concentrations, respectively.
The principal features of the Improved Low Temperature Digestion (ILTD) Process are as follow:
- no predesilication is needed
- digestion temperature about 150 °C
- high digestion A/C ratio, A/C ≥ 0.820 (AH ≤ 6 g/l, preferably ≤ 3 g/l), short digestion retention time, about 3-5 mins
- separation of the low soda bauxite residue just after the dissolution of gibbsite, preferably with pressure decanter and/or Hyperbaric (Hi-Bar) filtration, at about the digestion temperature
- seeded pressure crystallisation of the Desilication Product (DSP) out of the liquid phase.
Updated ILTD process
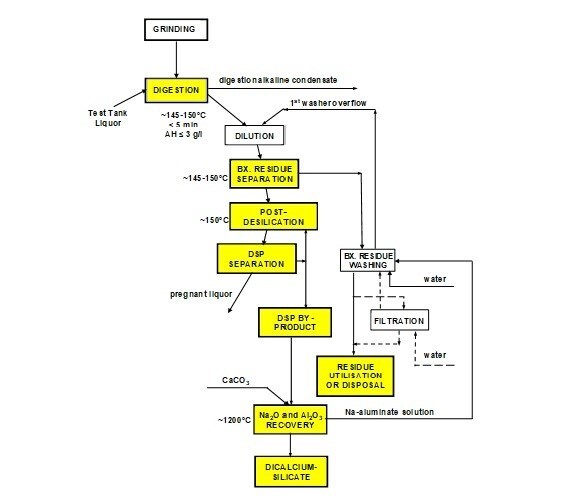
- The chemical composition of the DSP by-product from the ILTD Process is almost identical with nepheline mineral. Some unit operations of the processing of nepheline (similarly to other sintering processes) can be well utilised for processing of DSP. Based on the long experiences with processing of nepheline in Russia about 88 per cent of alumina and 92 per cent of soda content of the DSP (sodalite) by-product of the ILTD Process can be recovered by a small sintering-leaching unit. The sodium aluminate solution obtained from the leaching can be reused in the Bayer circuit. The dicalcium-silicate (belite, C2S) by-product of the sintering-leaching process step is welcome in the cement industry. The ILTD Process completed with the soda and alumina recovery from the DSP by-product by a sintering-leaching is re-named as Updated ILTD (UILTD) Process. „Bánvölgyi, Gy. (2021)”, „Bánvölgyi, G. and Nandi, A. (2022)” It may be emphasised that the alumina that is being recovered from DSP was originally in kaolinite, and this alumina is rightfully not considered recoverable in the Conventional Bayer (CLTD) process.
- In the figure, the blocks highlighted in yellow indicate the modified unit operations or the by-products of the Updated ILTD Process that are different from the CLTD process.
Process calculations
Process calculations of tentative chararacter were carried out for three alumina refineries located at the Eastern side of India. The amount and composition of the bauxite feedstocks, the bauxite residues, the same for the dicalcium-silicate (C2S, belite) by-products were calculated and presented for Conventional Low Temperature Digestion (CLTD) and compared with the Updated ILTD Process. The calculation results are shown in the Table 1 and Tables 3-5 for the NALCO Damanjodi, Hindalco Utkal and Vedanta Lanjigarh alumina refineries, respectively. For the general calculation purpose, defined bauxite qualities and mineralogies are assumed for these 3 alumina refineries. They do not reflect the exact bauxite qualities being used in these plants. Similarly for the estimation of COP, an approximate landed cost of bauxite, caustic soda and other raw materials are assumed for the comparative study purpose.
As observed, Na2O content of the Bauxite residue (BR) of the UILTD Process is well below 1 per cent, the Fe2O3 content is higher, therefore it is more suitable for various useful purposes such as being an additive in the making of Ordinary Portland Cement, in making iron, and/or artificial soil than BR of the CLTD. The dicalcium-silicate is welcome in the cement industry in large quantities.
Economic calculations
For each alumina refineries the Specific Material and Energy Consumptions, the items of the Cost of Production (COP) were calculated for the Conventional Low Temperature Digestion (CLTD) Process.
The Material and Energy cost savings for the Updated ILTD Process were calculated separately. The Coverage, i.e. the difference of the Selling price and the COP, the Investment cost estimates and the Payback periods for the three alumina refineries are summarised in Table 2. The selling price of alumina is assumed here as USD450 per ton for comparative results. It needs to be pointed out that the Payback periods were arrived at 2.5, 3.0 and 1.9 years, respectively, which are deemed to be favourable values.
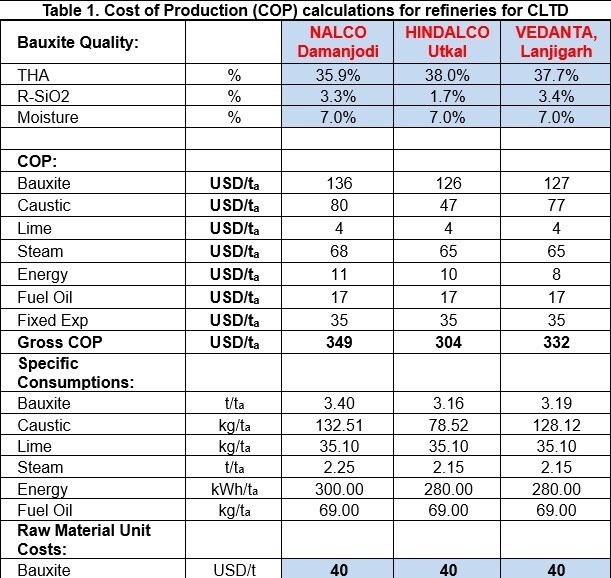
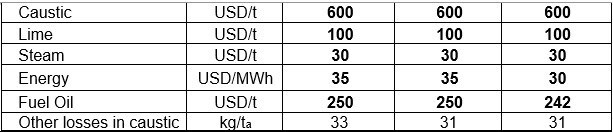
Table 2. Summary for the tentative economic calculations
References
Bánvölgyi, G., 2021, November. The Improved Low Temperature Digestion (ILTD) Process and its Recent Developments. In Proceedings of the 39th International.
ICSOBA Conference, virtual conference (pp. 99-111).
Bánvölgyi, G. and Nandi, A., 2022, September. The Improved Low Temperature Digestion (ILTD) Process for High Silica Bauxites and Aluminous Laterites. In Proceedings of 10th IBAAS International Conference (pp. 34-49).
Bárdossy, G. and Aleva, G.J.J., 1990. Lateritic bauxites. Developments in economic geology. Amsterdam: Elsevier, 27, p. 572
Komlóssy, Gy., 2021, Personal Communication, 29 July 2021.
Lyew-Ayee, P., 1997. Bauxite reserves for the world aluminium industry: Perspects to the year 2020. In The 8th International Congress of the International Committee for Study of Bauxite, Alumina & Aluminium (ICSOBA)-“Energy and Environment in the Aluminium Industry., Milan, Italy, 16-18 April, 1997, Proceedings, Part II, No 29, (pp. 9-31).
To learn exclusive industry data, download our reports here
This article is credited to György Bánvölgyi, Senior Process Consultant, and Dr. Ashok Nandi, President of the International Bauxite, Alumina & Aluminium Society (IBAAS).
Unlock full access – sign up for FREE.
Key benefits
World alumina production aligns with demand forecast, with a 6% growth in Q3 2025
Next articleChina's alumina production with 8% growth rate races ahead of primary aluminium, signalling surplus pressure
Grow with
AL Circle






















