“The template for each Electrically Heated High Convection Oven (EHKO) furnace zone is the preheating section of the extrutec gas furnaces, which extrutec has been using for many years.” Uwe Günter, CEO, extrutec GmbH
- Category
- Interview
- Date
- 12 September 2023
- Source
- AlCircle.com
AL Circle: You have developed an Electrically Heated High Convection Oven (EHKO) to curb carbon emissions, provided the oven is operated with ‘Green’ electricity. What is the minimum amount of carbon this equipment emits, and how less is it compared to average carbon emissions?
Uwe Günter: This system (provided that “Green” electricity is available) is more or less operated without curbing carbon emissions. All electric consumers are trimmed on the highest possible efficiency. The complete system reaches an efficiency of up to 87%.
All consumers have electric drives or are electrically operated like the heating elements.
Unlike other electrical stand-alone solutions, this new furnace type can be integrated into an existing process without additional handling and can, therefore, replace an existing furnace one-to-one. For a completely new investment, it is necessary to consider using an induction furnace, which provides for applying a taper. Optionally, the induction furnace can also be offered as an inline version (directly after the EHKO). We have applied for a worldwide patent on this.
Existing extrutec standards are used to implement this new type of furnace. The template for each EHKO furnace zone is the preheating section of the extrutec gas furnaces, which extrutec has been using for many years. Based on the extensive experience with this system, some minor improvements were incorporated to optimise the flow dynamics. The electrical heating elements are derived from similar elements used in previously supplied ageing or die ovens.
With this heating concept, we talk about a consumption of 148 kWh/t of electricity.
By comparison, even a fully optimised gas-fired furnace system equipped with all available preheating elements consumes at least 150 kWh/t of gas on average.
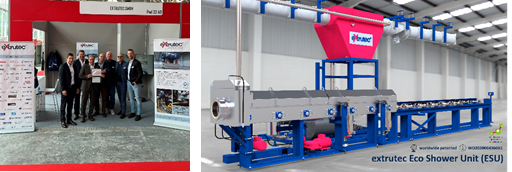
AL Circle: Please brief us on your Metef Innovation Award-winning Eco Shower Unit. What is its utility in Log Preheating?
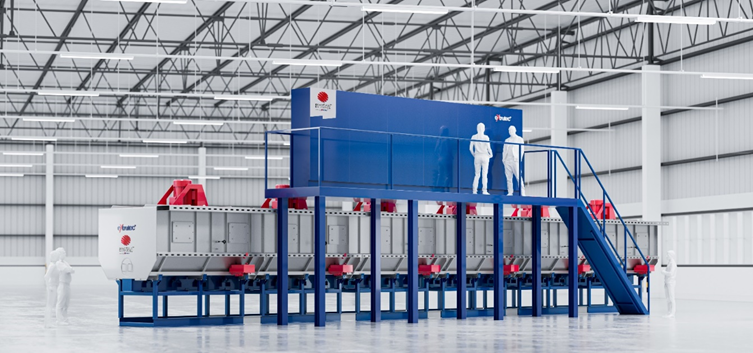
Uwe Günter: The extrutec ESU system (Eco Shower Unit) initially uses the waste heat from gas-heated furnaces, the coil cooling of the induction furnaces or also other external heat sources to heat water to just below boiling point (max. approx. 90°C). The system is connected directly upstream of the furnace systems (gas-heated systems, electrically resistance-heated (EHKO) or gas-heated) high convection system for the basic heating of the bars/billets in line. This preheats the pre-material to almost 90°C without significant additional energy input. This improves the overall efficiency of a heating plant by up to 18%. This worldwide recognised patent results in extrutec heating systems having the highest efficiency of all available systems.
AL Circle: Describe the technologies used in your heat treatment equipment. Are they backed by digital solutions?
Uwe Günter: For all our heating and heat treatment solutions, we try to reach the following:
- Preheating of logs/billets through heated water.
- High convection preheating for gas-fired furnace systems.
- Increasing the convection section length improves the energy efficiency of gas-fired furnace systems.
- Use of purely electrically operated heating systems.
- Use of waste heat from coil cooling of induction furnaces for preheating of aluminium logs/billets.
We have two kinds of digital solutions. The one is directly integrated into our equipment. The machine programs are designed to recognize and react flexibly to accommodate production situations. An example of this is our zone shutdown. If a production operation is run with only low throughput, we shut down a direct heating zone in order to save energy. We switch off a direct heating zone to save energy.
In addition, we are currently developing a digital solution to evaluate production and machine data both online and offline and thus generate added value for the various stakeholders in the extrusion plant. The first machines are already equipped with this solution and can display live and archive data via the Internet from anywhere.
AL Circle: How do modern technologies and equipment benefit the aluminium heat treatment process?
Uwe Günter: Lower energy consumption, reduction of the scrap rate, increase in output through higher press speeds (reproducible taper), reduction of the weights per metre, reduction of the proportion of alloying elements through optimised heat treatment and profile cooling processes => productivity increases through all the aforementioned process optimisations.
AL Circle: What is the Eco Heating Process? How do you define an energy-optimized heating process? Please elaborate.
Uwe Günter: The extrutec EHPTM - The Eco Heating Process describes the world's most efficient gas-based heating process. The process consists of three stages.
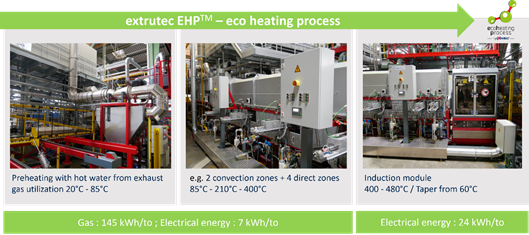
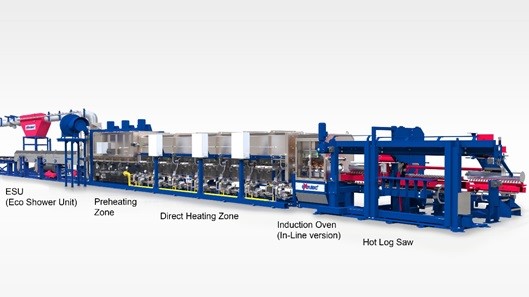
Stage1 consists of preheating the aluminium logs or billets with approx. 85 - 90°C warm water. The water is heated either by using the exhaust heat from gas-fired furnaces, heat from the coil cooling of the induction furnaces or even by using external heat (anodising plants, foundries, hydraulic plants).
Stage 2 is the basic heating of the logs/billets to approximately a basic axial temperature. 400°C. Either a gas-heated furnace or, since September 2023, a purely electrically heated high convection furnace (EHKO) is used for this.
Stage 3 then includes the induction furnace (inline or stand-alone) for producing an absolutely reproducible taper. The induction furnace is characterised by far the highest achievable temperature gradients in the heating range. In addition, with this heating technology, there is continuous temperature measurement during the heating process, which is not the case with all heating technologies.
AL Circle: What futuristic technical developments might the global aluminium heat treatment process require?
Uwe Günter: The most important requirements for all heating systems used in the field of aluminium extrusion technology are:
- Max. possible energy efficiency for the permanent improvement of the carbon footprint.
- Absolute reproducibility with regard to temperature control and tolerance.
- Very fast temperature changes, especially for small batch sizes.
- For gas-fired systems, a quick changeover option from natural to liquid gas.
AL Circle: The equipment you offer for heat treatment is appropriate for the downstream aluminium products. Do you plan to design any equipment for the upstream sector or recycling?
Uwe Günter: We are not planning any plant developments in the foundry or melting area of Al-logs and billets, as well as recycling products. However, our subsidiary, TCT Induktionstechnik GmbH, is very successful in the service and repair of induction equipment from the foundry sector.
TCT takes care of all service issues for foundry technology. We can service, repair or remanufacture all induction coils from any manufacturer. In addition, we have already completely replaced many switchgear of various induction applications.
Our goal is always to be close to our customers and help them in the best possible way.
